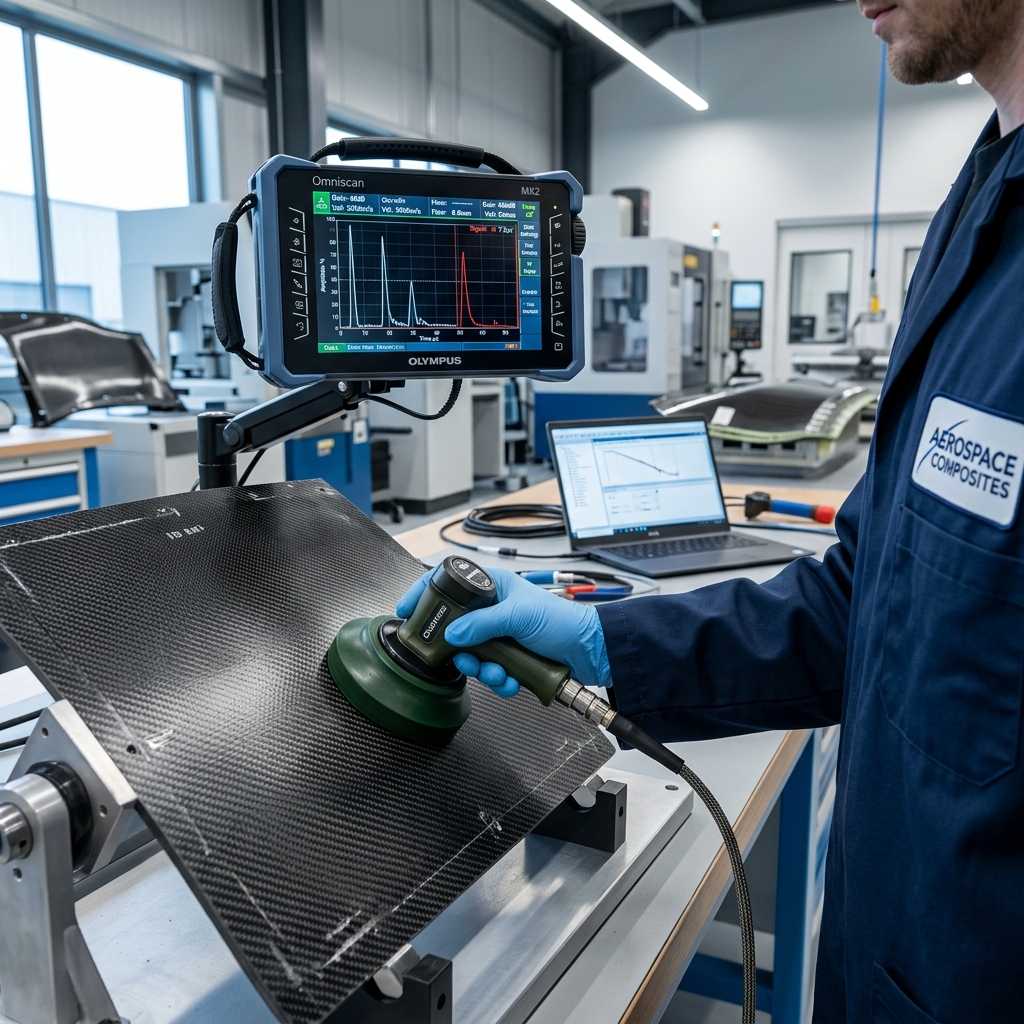
Dry-Coupled Ultrasonic Testing (DCUT)
Method Overview
Dry-contact ultrasonic testing utilizing elastomeric film transducers for non-contaminating composite, wood, and metal testing.
Core Method Specifications
Target Applications & Governing Standards
1 Scopes ConfiguredMethod Limitations & Operational Boundary Conditions
Critical physics limits, thermal envelopes, blind spots, and ASME Sec V / API procedural boundaries for DCUT.
Elastomeric dry-coupling pad degrades and hardens if exposed to excessive surface temperatures.
Near-surface dead zone reduced to < 1.0 mm with high-damped elastomeric delay lines
ZERO LIQUID (uses proprietary dry elastomeric acoustic impedance matching membrane)
Transducer face must maintain firm perpendicular contact with surface under controlled mechanical pressure
- •Extremely rough or porous cast surfaces that puncture or shred the thin dry-coupling elastomer film
- •High acoustic attenuation in un-compacted thick composite laminates
Uneven operator hand pressure on probe creating variable coupling loss mistaken for delamination
Laser shearography for rapid full-field disbond mapping without point-by-point contact
Optical inspection of internal core edges and hollow cavity walls
Technique-to-OEM Compatibility Matrix
Verified manufacturers, instrument models, and diagnostic portals supporting DCUT.
Evident Scientific
Global leader in advanced optical, ultrasonic, and radiographic inspection technologies (formerly Olympus Scientific Solutions).
Innerspec Technologies
World leader in Electro Magnetic Acoustic Transducer (EMAT) technology and dry-coupled ultrasonic testing (DCUT) for high-temperature and couplant-free inspection.
Sonatest
Pioneering British manufacturer of rugged ultrasonic flaw detectors, phased array instruments, wheel probes, and precision UT transducers.
Modsonic Instruments
Pioneer Indian manufacturer of portable ultrasonic flaw detectors, thickness gauges, and transducers with 35+ years of indigenous NDT engineering.