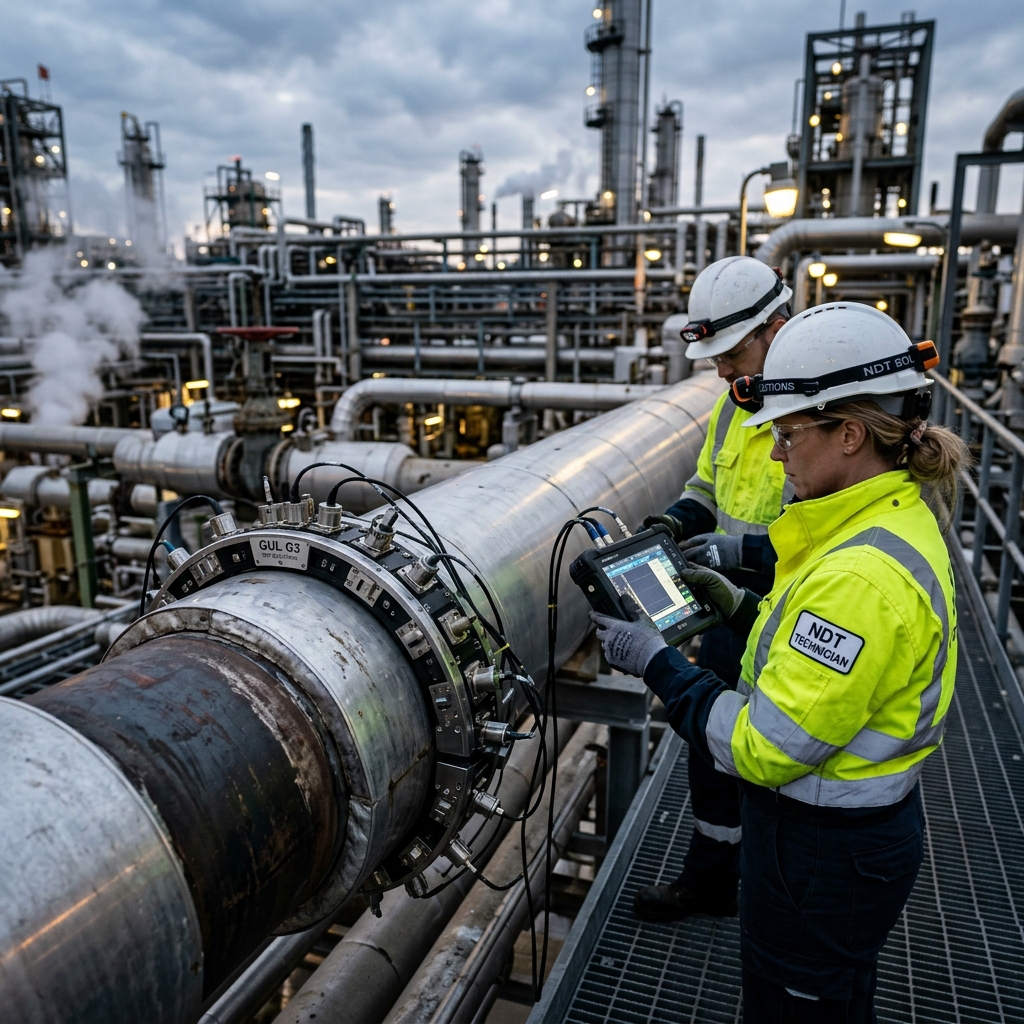
Guided Wave Testing (GWT)
Method Overview
Long-range screening of pipelines and structural piping using low-frequency ultrasonic waves guided by structural boundaries.
Core Method Specifications
Target Applications & Governing Standards
1 Scopes ConfiguredMethod Limitations & Operational Boundary Conditions
Critical physics limits, thermal envelopes, blind spots, and ASME Sec V / API procedural boundaries for GWT.
Acoustic wave dispersion curves shift with metal temperature, requiring recalculated torsional/longitudinal wave mode velocity tables.
Transducer collar near-field dead zone masks first 0.5 m to 1.5 m (1.6 to 5.0 ft) on either side of ring
Dry mechanical pneumatic pressure clamping or light couplant pads
Excellent for detecting circumferentially oriented metal loss bands; insensitive to isolated narrow axial pinholes
- •Localized deep pinhole pitting: Discontinuities covering < 3% of total cross-sectional area (CSAC) cannot be resolved
- •Axially oriented narrow gouges or tight cracks parallel to sound propagation vector
- •Piping sections immediately beyond heavy welded flanges, valve bodies, or solid soil burial transitions
Heavy external clamped pipe supports causing wave reflection signals that look like corrosion thinning
Follow-up spot UT or manual B-scan mapping on localized suspect zones flagged by GWT screening
Confirm wall loss through insulation without stripping full lines
Technique-to-OEM Compatibility Matrix
Verified manufacturers, instrument models, and diagnostic portals supporting GWT.
Eddyfi Technologies
Advanced non-destructive testing conglomerate encompassing Eddyfi electromagnetic arrays, Silverwing tank floor scanners, Teletest guided waves, Inuktun robotic crawlers, and M2M phased array instruments.
Guided Ultrasonics (GUL)
Imperial College London spinout and authoritative pioneer of long-range guided wave ultrasonic testing (GWT / LRUT) systems for rapid pipeline corrosion screening under insulation (CUI).
Plant Integrity
OEM Manufacturer for GWT inspection systems.
Teletest
OEM Manufacturer for GWT inspection systems.
FBS Inc
OEM Manufacturer for GWT inspection systems.